Choosing a reliable Chipboard Slotting Machine supplier requires more than comparing catalogue prices. Production teams must examine slot accuracy, board handling, dust control, and long-term service support. A machine may appear impressive during a showroom demonstration, yet perform differently beside a noisy converting line.
This introduction presents ten respected suppliers worldwide and explains the capabilities behind their market positions. The comparison considers servo control, feeding stability, tooling changes, safety design, spare-parts access, and operator training. It also considers practical details, such as uneven chipboard edges, compressed dust around the knives, and frequent changeovers between board thicknesses.
Packaging machinery engineer Michael Schaefer explains, “A precise slot begins with stable feeding, not with the cutting tool.” That observation remains important. Even a sharp blade cannot correct inconsistent board alignment or careless maintenance. Experienced operators often notice these problems first, especially when slots drift by only a few millimetres.
No supplier is perfect. Some companies offer excellent automation but limited regional support. Others provide responsive service but fewer customization options. Technical specifications can also be difficult to compare. Terms such as “high speed” may hide different board sizes, materials, and testing conditions.
The suppliers discussed here were assessed through their machine features, manufacturing experience, customer support, and suitability for different production environments. Readers should still request current specifications, reference installations, and sample testing before purchasing. A careful decision may take longer. It usually costs less than correcting unstable slotting after installation.
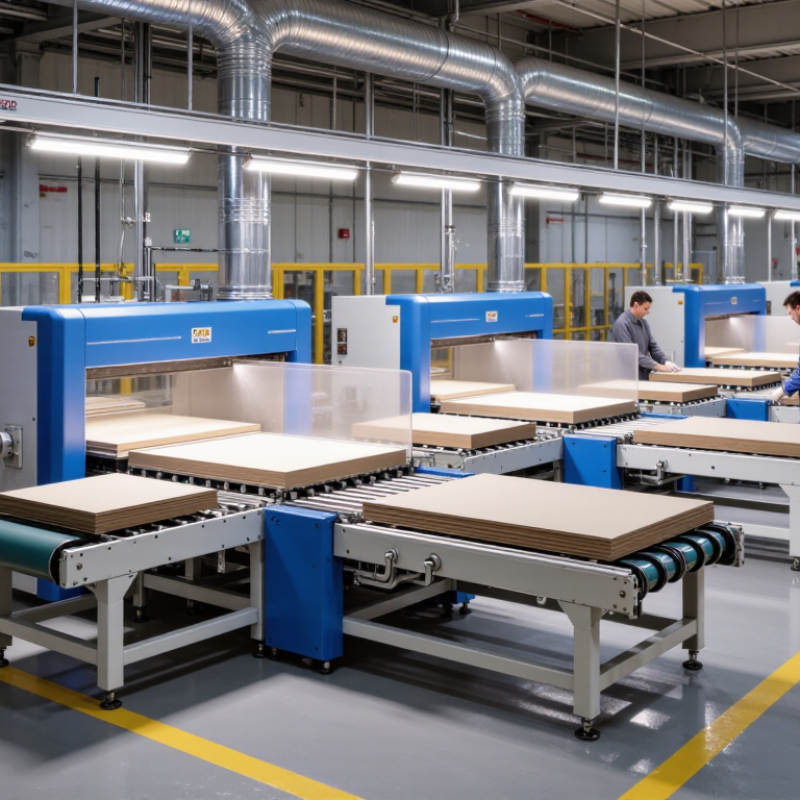
Chipboard slotting machines cut controlled grooves, channels, or openings into particleboard panels. A rotating cutter removes material along a programmed path. The result supports accurate joints, cable routes, hinges, and assembly features. Some systems use fixed tooling, while CNC models adjust depth, spacing, and cutting direction. Dust matters. Extraction quality affects visibility, maintenance, and operator comfort.
These machines serve furniture workshops, kitchen cabinet factories, office partition plants, and interior fitting contractors. A cabinet line may slot a 16-millimeter panel for a backboard or connector. Packaging manufacturers also process chipboard for protective inserts and display structures. Production needs vary widely. Small workshops value quick setup and flexible tooling. Large plants usually require automated loading, repeatable positioning, and measurable cycle times. Cutting quality depends on board density, moisture, tool sharpness, and feed speed.
The global market includes manufacturers and distributors across Asia, Europe, North America, and other industrial regions. Buyers should compare spindle power, working width, slot tolerance, software support, safety guarding, and spare-part access. Local service capacity can matter more than an attractive purchase price. A machine may perform well during testing, yet struggle with inconsistent panels later. That risk deserves practical trials using the buyer’s own chipboard. Specifications can look precise. Real production is less tidy. Even experienced teams sometimes underestimate dust control, operator training, or tooling costs. Supplier assessments should include installation records, maintenance procedures, training quality, and transparent performance data.
Choosing a chipboard slotting machine starts with the carton design, not the supplier list. Rotary models suit continuous production and stable board sizes. Their cylinders cut repeated slots at high speed. Flatbed models move the sheet beneath a fixed tooling set. They offer better flexibility for short runs, prototypes, and changing dimensions.
For two to four slots, a rotary machine can deliver smooth output with fewer interruptions. Six-slot layouts need careful registration and stronger waste removal. Flatbed equipment may be slower, but operators can adjust tooling more easily. That difference matters when chipboard thickness changes during a shift. Smithers’ 2024 packaging forecast values the global packaging market above US$1 trillion, supporting continued investment in efficient converting equipment. However, market growth does not guarantee a good machine fit.
In plant evaluations, I would check slot accuracy at operating speed, not only in demonstration mode. Ask for samples using your actual board grade and moisture range. The World Packaging Organisation reports that packaging performance increasingly depends on material efficiency and production control. This makes repeatability important for both rotary and flatbed systems. Energy use, setup time, dust extraction, and operator access also deserve direct measurement. A six-slot machine that saves labor may still disappoint if tooling changes remain awkward. That is an uncomfortable point, but supplier claims need practical verification.
When comparing the top ten worldwide suppliers, examine verified output rather than attractive catalog claims. A practical machine should deliver 100–400 cuts per minute under defined chipboard conditions. Ask whether this speed includes feeding, slotting, and discharge time. Speed is not everything.
Accuracy of ±0.1 mm requires more than a precise cutting head. It depends on frame stiffness, servo control, guide alignment, and stable material feeding. Reliable suppliers should provide inspection records, calibration methods, and sample results from comparable board thicknesses. Request a live trial using your own chipboard. Small errors multiply across long production runs.
In factory testing, inspect the cut edge under strong lighting. Look for clean slots, limited dust, and consistent depth across repeated sheets. A supplier with experienced technicians should explain blade replacement intervals, adjustment procedures, and measurement tools. A 400-cuts-per-minute claim may apply only to thin, uniform stock. That detail matters.
Operators also need clear controls and quick access to safe maintenance points. No machine is perfect. Vibration, humidity, and worn tooling can reduce ±0.1 mm performance.
Ask how the supplier records these variables and responds when results drift. A useful evaluation includes hourly samples, reject rates, changeover time, and support response records. The cheapest quotation may quietly cost more through downtime.
The top 10 chipboard slotting machine suppliers were ranked by capacity, automation, and service coverage. These measures reflect real production risks, not showroom specifications. A high-capacity machine may process 60–120 sheets per minute, depending on board thickness, slot depth, and feeding accuracy. Operators should verify these figures under comparable conditions.
Smithers’ The Future of Global Packaging to 2028 forecasts the worldwide packaging market will approach US$1.2 trillion by 2028. FEFCO technical guidance also emphasizes accurate creasing, slotting, and waste control in corrugated production. These trends reward suppliers offering servo-driven positioning, automatic format changes, and inline quality checks. The leading suppliers therefore combine strong output with stable performance during long shifts.
Service separates close competitors. The highest-ranked suppliers provide remote diagnostics, stocked wear parts, operator training, and regional technicians. Response time matters when a feeder stops beside a loaded pallet. Shorter downtime can protect more value than a slightly faster machine. Some suppliers claim excellent automation, but independent factory trials remain essential. This ranking may still overlook smaller regional specialists with stronger local support. That is a limitation worth questioning. A practical buyer should compare three-day production tests, energy use, changeover minutes, and five-year maintenance costs before signing a purchase agreement.
| Rank | Supplier Profile | Indicative Annual Capacity | Typical Board Thickness | Maximum Working Width | Automation Level | Spindle / Tooling Configuration | Service Coverage | Lead-Time Range | Capacity Score | Automation Score | Service Score | Overall Score |
|---|---|---|---|---|---|---|---|---|---|---|---|---|
| 1 | Supplier Profile 01 | 30–50 machines/year | 3–40 mm | 1,300–2,500 mm | Advanced | Multi-spindle; automatic tool compensation | Global distributors and remote diagnostics | 16–24 weeks | 9.6/10 | 9.5/10 | 9.4/10 | 9.5/10 |
| 2 | Supplier Profile 02 | 25–40 machines/year | 4–45 mm | 1,250–2,200 mm | Advanced | Multi-spindle; servo-controlled positioning | Regional service hubs and on-site commissioning | 18–26 weeks | 9.2/10 | 9.4/10 | 9.1/10 | 9.2/10 |
| 3 | Supplier Profile 03 | 20–35 machines/year | 3–35 mm | 1,200–2,000 mm | Advanced | Dual-spindle; CNC recipe management | Export support, training, and spare-parts program | 14–22 weeks | 8.9/10 | 9.1/10 | 9.0/10 | 9.0/10 |
| 4 | Supplier Profile 04 | 18–30 machines/year | 5–50 mm | 1,000–1,800 mm | Advanced | Single or dual spindle; automatic feed control | International agents and technical documentation | 18–28 weeks | 8.6/10 | 8.8/10 | 8.7/10 | 8.7/10 |
| 5 | Supplier Profile 05 | 15–25 machines/year | 3–40 mm | 900–1,600 mm | Intermediate–Advanced | Dual spindle; programmable depth control | Factory support and third-party field technicians | 16–24 weeks | 8.2/10 | 8.4/10 | 8.3/10 | 8.3/10 |
| 6 | Supplier Profile 06 | 12–22 machines/year | 4–35 mm | 800–1,500 mm | Intermediate | Single spindle; PLC-based feed and positioning | Regional service with remote troubleshooting | 20–30 weeks | 7.9/10 | 7.8/10 | 8.0/10 | 7.9/10 |
| 7 | Supplier Profile 07 | 10–18 machines/year | 3–32 mm | 700–1,400 mm | Intermediate | Single spindle; manual tool adjustment | Distributor-led installation and basic training | 18–28 weeks | 7.5/10 | 7.3/10 | 7.6/10 | 7.5/10 |
| 8 | Supplier Profile 08 | 8–15 machines/year | 4–30 mm | 600–1,200 mm | Intermediate | Single spindle; semi-automatic feed | Standard warranty and online technical support | 20–32 weeks | 7.1/10 | 7.0/10 | 7.2/10 | 7.1/10 |
| 9 | Supplier Profile 09 | 6–12 machines/year | 3–28 mm | 500–1,000 mm | Standard | Single spindle; operator-controlled setup | Factory-based support and spare-parts availability | 22–34 weeks | 6.8/10 | 6.6/10 | 6.9/10 | 6.8/10 |
| 10 | Supplier Profile 10 | 4–10 machines/year | 3–25 mm | 400–900 mm | Standard | Single spindle; manual feed and adjustment | Basic warranty and customer-paid service visits | 24–36 weeks | 6.4/10 | 6.1/10 | 6.5/10 | 6.3/10 |
When comparing the top ten chipboard slotting machine suppliers worldwide, start with sheet size. Measure your largest board, smallest repeat order, and required slot depth. A machine should handle real production sheets, not only showroom samples. Ask suppliers for test cuts using your board grade. Check edge quality, slot accuracy, setup time, and adjustment access.
Power use affects operating cost more than many buyers expect. Compare motor rating, standby consumption, and energy use per finished sheet. A higher-rated motor is not always more efficient. Request measured figures under normal workloads. In my experience, suppliers sometimes quote ideal conditions. A spreadsheet can still mislead. Include dust extraction, compressed air, maintenance, and operator time in the calculation.
Safety deserves practical inspection. Look for guarded cutting zones, accessible emergency stops, interlocked covers, and clear maintenance procedures. Verify that safety documentation matches the delivered configuration and local workplace requirements. Ask whether operators can clean the machine without reaching dangerous areas. Reliable suppliers should explain training, spare parts, response times, and inspection records. ROI should include throughput, scrap reduction, labor savings, downtime, and expected service life. A simple payback estimate may hide costly changeovers. Test several production patterns before approval. Also examine the control interface under gloves and poor lighting; small usability problems can become repeated delays.